Study capability only after the process and measurement method are defined
Choose a measurable characteristic with engineering-based upper and lower specification limits, verify that the measurement system is suitable, collect time-ordered production data from a stable process and review the distribution before interpreting Cp or Cpk. Use the result as process evidence, not as a substitute for product identification, control plans or shipment release.
1. Start with the Cp and Cpk capability study decision
Choose a measurable characteristic with engineering-based upper and lower specification limits, verify that the measurement system is suitable, collect time-ordered production data from a stable process and review the distribution before interpreting Cp or Cpk. Use the result as process evidence, not as a substitute for product identification, control plans or shipment release.
A useful buying decision begins with the exact product configuration and customer task, not a generic claim about LED boards. For this topic, the controlled subject is the statistical relationship between a stable production process and the specification limits for a critical LED acrylic board dimension. Record panel thickness, base-slot width, panel-to-base clearance, cut dimension, fixture and instrument, time order and process stream before comparing samples. Those facts determine whether two units are genuinely comparable and prevent a visible difference from being attributed to the wrong material, component, power source, or process. This record remains specific to the Cp and Cpk capability study decision.
This guide uses Cp and Cpk capability study as a practical B2B control method. It does not claim that LumDigi, a model, a factory or a shipment is certified to an industry-specific system unless current project evidence explicitly supports that statement. The review should therefore separate three questions: what the buyer needs, what the identified sample actually demonstrates, and which conclusion still requires qualified engineering, laboratory, or destination-market review. That separation gives procurement teams a defensible basis for a request for quotation without turning a short sample observation into a lifetime, safety, or compliance promise. This record remains specific to the Cp and Cpk capability study decision.
Before contacting suppliers about Cp and Cpk capability study, assign an owner to the commercial need, an owner to the technical evidence, and a person authorized to accept a trade-off. Give them the same one-page brief and require each comment to reference the sample code or specification field. This simple handover matters when the importer, brand, testing adviser, inspection company, and factory work in different locations. It prevents a merchandising preference from being reported as a regulatory rule and prevents an unresolved technical question from disappearing inside a general approval. Record the final decision, evidence reviewed, open items, and next review trigger in language a future replenishment team can understand. This record remains specific to the Cp and Cpk capability study decision.
- Name the exact model, panel, base, cable, marker set, and operating condition involved.
- Use a capability conclusion supported by valid limits, a suitable measurement system, rational production data, stability review and an agreed buyer action as the commercial decision rule.
- Record unknowns rather than filling them with catalogue assumptions.
2. Understand what can change the result
Cp compares potential process spread with the specification width, while Cpk also reflects how the process mean is positioned between the limits. Both can mislead when the process is unstable, the distribution is unsuitable or the measurement variation is large.
Cp and Cpk capability study depends on the complete identified configuration
NIST explains process capability as a comparison between an in-control process and specification limits, and presents Cp and Cpk as indices based on process spread and centering. A buyer does not need to reproduce a material-science laboratory to manage this risk, but the quotation and sample plan must identify the variables that the factory controls. Ask which inputs are fixed by drawing or bill of materials, which depend on the production route, and which can vary with environment or operator technique. This record remains specific to the Cp and Cpk capability study decision.
Primary technical references in this guide explain the general mechanism or measurement scope; they do not certify a LumDigi model or create a universal acceptance limit. Use them to ask better questions, then rely on product-specific drawings, supplier declarations, samples, and suitable test evidence. This is especially important when a method developed for sheet material, a connector, a lamp, or an art material is being used only as context for a finished drawing-board assembly. This record remains specific to the Cp and Cpk capability study decision.
- Identify the mechanism and the buyer decision before choosing a test.
- Keep panel thickness and base-slot width visible in the evidence record.
- Use external references as context, not as certification of a LumDigi product.
3. Build a sample matrix before testing
Compare controlled configurations that isolate the variables most likely to change the Cp and Cpk capability study result.
Use one identified product family and follow representative units through the actual acrylic-panel, LED-base, assembly, function-check and packing flow. Include ordinary output and at least one known change or exception scenario so the Cp and Cpk capability study workflow can be tested before order release. Give each unit a sample code and retain the configuration record with photographs taken before the review. If a supplier proposes an alternate input, make it a separate matrix row rather than silently replacing the approved reference. This protects the buyer from approving one combination and receiving another. This record remains specific to the Cp and Cpk capability study decision.
Keep the matrix small enough to interpret. Change one significant variable at a time where practical, while holding product revision, bill of materials, sample identity, work sequence, measurement method, acceptance reference and decision owner constant. Include a repeat unit when the commercial risk is lot consistency rather than a one-off demonstration. A buyer sample is evidence for a defined decision; it is not automatically a statistically representative production result. This record remains specific to the Cp and Cpk capability study decision.
- Use coded samples and retain an untouched reference.
- Change one important variable at a time where practical.
- Record the actual product, setup and environment beside every result.
4. Use a repeatable review method
Use a written, repeatable method that reproduces the buyer's actual decision conditions without turning an in-house review into an unsupported certification claim.
Map the physical flow, observe the work at the point where evidence is created, compare the record with identified samples, and run one traceable review from customer requirement through disposition. Keep actual observations separate from assumptions and close every action through a named owner. Write the sequence before viewing the result so observers do not change the method after seeing a preferred sample. Record setup, duration, handling, power source, room condition, and any cleaning or reset step that could influence the next observation. This record remains specific to the Cp and Cpk capability study decision.
Capture raw time-ordered values, stability signals, mean and spread, distribution shape, Cp/Cpk estimate and confidence. Use neutral photographs and short unedited video where motion or control behavior matters, and label every file with the sample code. Do not enhance glow, hide a defect with exposure, or crop away the cable and base when those elements are part of the question. Installation preparation should use only the proposed accessories and a stable, ordinary application setup. This record remains specific to the Cp and Cpk capability study decision.
- Photograph the starting condition before handling or adjustment.
- Use one defined sequence, observation distance and operating condition.
- Keep files traceable to the sample code and reviewer.
5. Interpret observations without overclaiming
Interpret the recorded evidence against the stated customer requirement and preserve open questions for the appropriate technical, legal or laboratory reviewer.
A sample review can show whether the observed configuration meets the buyer's stated task under recorded conditions. It cannot by itself establish every production unit, every environment, or an unspecified service period. Do not convert a planning worksheet, one successful pilot, a capability number, a concession or an internal disposition into a universal promise about compliance, safety, lifetime or every future production lot. If the buyer needs a measured value or regulated conclusion, define the applicable method, specimen, equipment, laboratory competence, and report before assigning a limit. This record remains specific to the Cp and Cpk capability study decision.
Use three result states: accepted for the defined purpose, rejected against a written criterion, or open pending evidence. Avoid labels such as premium, safe, durable, uniform, or compliant unless the claim has a defined meaning and support. Where two configurations both work, preserve the trade-off rather than forcing a winner. The best sourcing choice is the one that meets the customer requirement with controllable production and truthful product communication. This record remains specific to the Cp and Cpk capability study decision.
- Separate preference, functional acceptance and measured evidence.
- State the configuration and limitations beside the result.
- Reopen approval after a relevant material, process or component change.
| Decision field | Record in the buyer file |
|---|---|
| Requirement | Exact characteristic, customer need, revision and acceptance boundary |
| Control evidence | Process step, owner, method, frequency, record and reaction |
| Release | Open point, disposition authority, due date and retained evidence |
6. Translate the decision into the RFQ
Turn the accepted Cp and Cpk capability study condition into explicit RFQ fields, sample references, evidence requests and change-notification rules.
The RFQ should identify characteristic and limits, measurement method, data period and source, stability evidence, capability method, reaction threshold and owner. Attach the sample matrix, approved photographs, and any drawing or artwork revision needed to make those fields unambiguous. Ask the supplier to mark confirmed, conditional, optional, and unsupported points. This produces comparable quotations and prevents an attractive reference image from becoming an unintended specification. This record remains specific to the Cp and Cpk capability study decision.
Request the proposed evidence with the quote: material or component identity, current datasheet where relevant, sample lead time, change-notification route, and the inspection checkpoint that will confirm production. Use LumDigi's custom design process for shape and presentation discussions, review a relevant shaped LED board reference, and send the controlled brief through the B2B enquiry page. Availability and final specifications must be confirmed for the selected model. This record remains specific to the Cp and Cpk capability study decision.
- Require a response against every named field.
- Attach approved sample photographs and document revisions.
- Mark confirmed, conditional, excluded and unresolved items separately.
7. Carry the approved condition into production
Hold the approved inputs and process conditions through incoming review, assembly and in-process verification, then document any authorized deviation.
Production control should cover stable setup, material and tool identity, measurement-system verification, time-ordered data, special-cause reaction, capability review. Link each checkpoint to a drawing, bill-of-material line, approved sample, work instruction, or recorded setting rather than relying on memory. If a change affects the mechanism discussed in this guide, pause and evaluate it against the approved decision before allowing the new condition into the order. This record remains specific to the Cp and Cpk capability study decision.
Factory testing should answer the commercial question with a repeatable method and traceable units. It should not be described as third-party certification unless it genuinely is. Retain representative evidence from start-up, in-process review, and the production lot where the risk justifies it. For a custom shape or private-label set, synchronize the panel, base, marker, cable, insert, and pack revisions so a correct component is not assembled into the wrong configuration. Compare the evidence plan with this related buyer guide before final approval. This record remains specific to the Cp and Cpk capability study decision.
- Link checkpoints to the bill of materials, drawing or work instruction.
- Retain start-up and in-process evidence from identified units.
- Route changes through written buyer approval when they affect the decision.
8. Verify the shipment-level evidence
Verify the agreed Cp and Cpk capability study evidence on identified finished units and connect findings to an authorized release, correction, reinspection or hold decision.
Shipment inspection can check correct characteristic and units, current limits, identified data source, stable-process evidence, buyer-approved interpretation, using the buyer's approved references and sampling instruction. The report should identify the lot, selected units, method, actual observations, photographs, limitations, and disposition. A pre-shipment check is valuable commercial evidence, but it does not replace material qualification, laboratory testing, or regulatory assessment required for the destination market. This record remains specific to the Cp and Cpk capability study decision.
When a finding occurs, describe it against the requirement and separate observation from cause. Define correction, reinspection, concession, or hold authority before shipment release. Archive the report with the purchase order, change notices, and approved sample. This creates a practical trace from customer requirements to production and reduces disputes built on unlabeled photos or recollection. This record remains specific to the Cp and Cpk capability study decision.
- Record the lot, variant, selected unit and method.
- Describe observations against the written requirement.
- Archive findings, corrections and final disposition together.
9. Conclusion: make Cp and Cpk capability study a controlled buying decision
Control Cp and Cpk capability study through a defined requirement, identified samples, repeatable evidence, production checkpoints and truthful claim boundaries.
The commercial value of Cp and Cpk capability study comes from connecting a buyer requirement to the process, evidence, reaction and authorized release decision without overstating what the record proves. The process is intentionally narrower than a broad product claim: define the need, compare identified configurations, record the method, and translate the decision into production and inspection controls. That sequence gives retail, distribution, and private-label teams information they can explain accurately to colleagues and customers. A supporting procurement guide can be used to align the adjacent buying decision without collapsing two specifications into one. This record remains specific to the Cp and Cpk capability study decision.
For LumDigi, send the target market, channel, preferred board shape, power arrangement, marker set, quantity scenario, packaging direction, and the specific Cp and Cpk capability study question. LumDigi can confirm facts for offered configurations and organize a relevant sample discussion. Buyers remain responsible for destination-market decisions and should use qualified reviewers where standards, safety, legal, or laboratory conclusions are required. This record remains specific to the Cp and Cpk capability study decision.
- Approve a complete configuration rather than an isolated photograph.
- Keep product, artwork, instructions and inspection evidence aligned.
- Reconfirm the decision after relevant changes.
Frequently asked questions
What should a buyer specify about Cp and Cpk capability study?
Specify characteristic and limits, measurement method, data period and source, stability evidence, capability method, reaction threshold and owner. Attach the identified sample and state which fields are requirements, preferences, or open questions.
Can one sample prove every Cp and Cpk capability study result?
No. A sample can support the defined decision under recorded conditions. Do not convert a planning worksheet, one successful pilot, a capability number, a concession or an internal disposition into a universal promise about compliance, safety, lifetime or every future production lot. Production consistency, lifetime, safety, and regulatory conclusions need evidence appropriate to those separate claims.
Which changes should trigger a new review?
Review changes to stable setup, material and tool identity, measurement-system verification, time-ordered data, special-cause reaction, capability review. The buyer and supplier should agree which changes require notification, a comparison sample, updated documents, or qualified assessment.
What belongs in shipment inspection?
The plan can verify correct characteristic and units, current limits, identified data source, stable-process evidence, buyer-approved interpretation against approved references. It should identify the lot, method, selected units, findings, limitations, and authorized disposition.
Image planning for this topic
These notes document the role and intended context of the two visuals used in this guide.
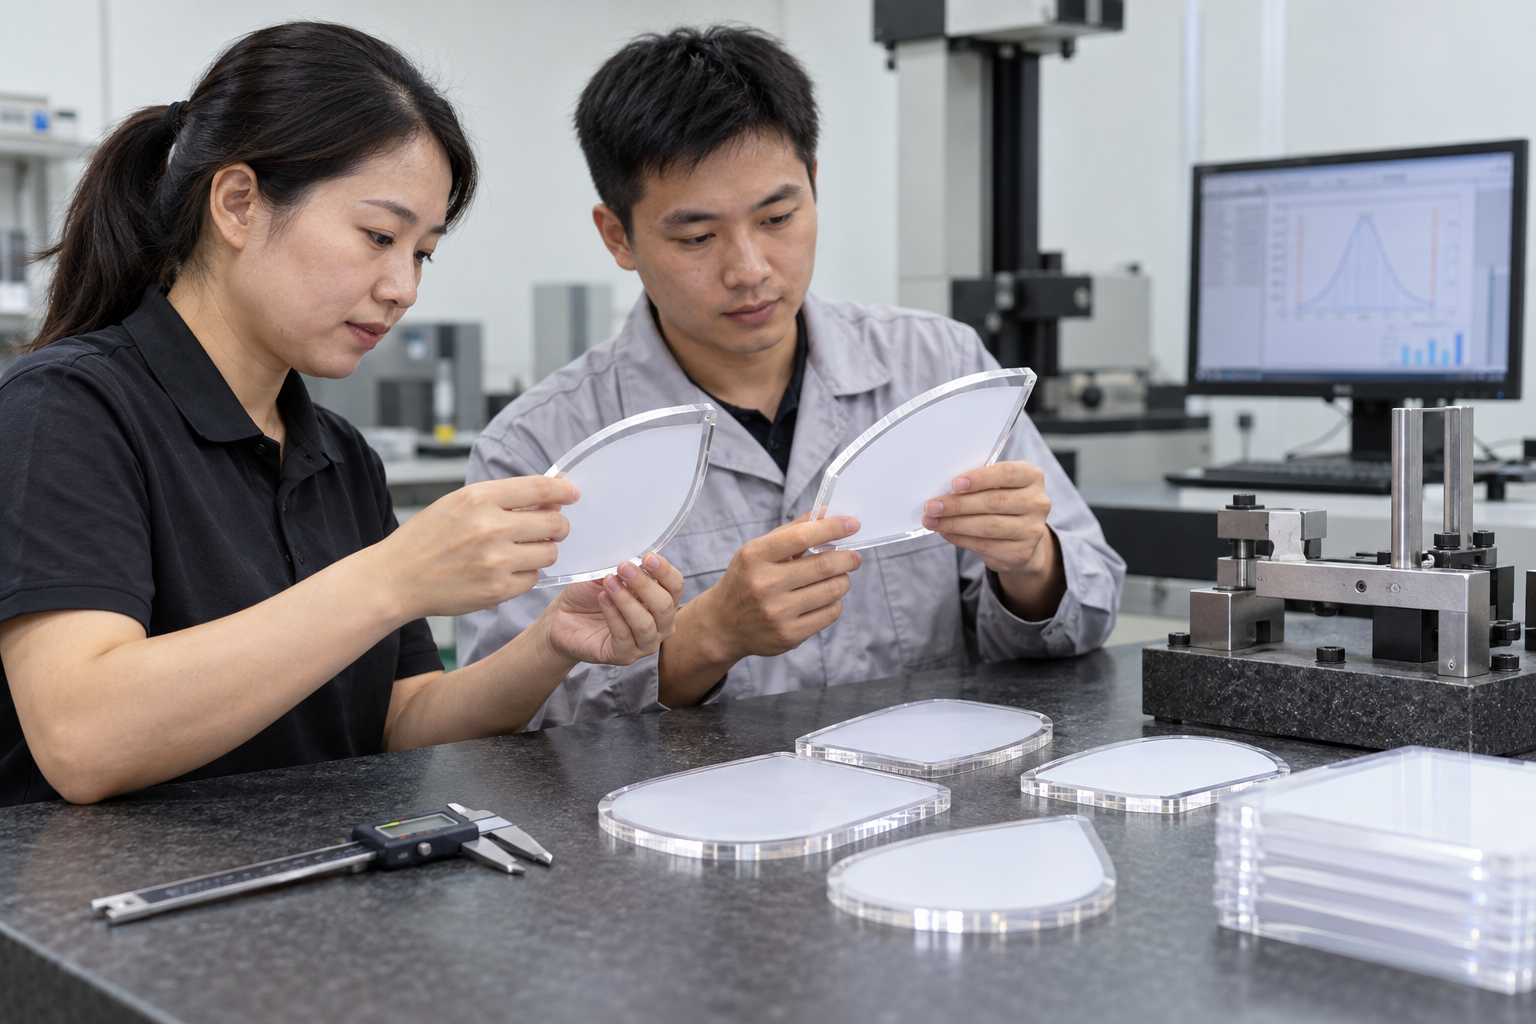
Show a controlled buyer review of Cp and Cpk capability study
- Placement
- hero
- Caption
- Illustrative AI-generated photograph: an Asian buyer and Chinese engineer compare identified Cp and Cpk capability study samples under controlled conditions.
- ALT text
- Asian buyer reviewing Cp and Cpk capability study samples for LED drawing boards
View AI image direction
Use case: photorealistic-natural. Asset type: editorial photograph for a LumDigi B2B LED acrylic drawing board technical guide. An Asian sourcing quality manager and Chinese metrology technician review coded shaped acrylic panels, a stable dimensional fixture and a non-readable capability plot in a clean measurement room. Landscape 3:2 composition, candid documentary commercial photography, natural modest lighting, realistic transparent acrylic, restrained plausible LED glow, genuine workshop or sample-room texture, believable anatomy. If employees appear, every employee is a Chinese/Asian adult. No invented logos, certification marks, readable documents, readable instrument values, numerical test results, watermark, or text overlay. This is an illustrative planning scene, not proof of an actual LumDigi test, factory result, shipment, or customer project.
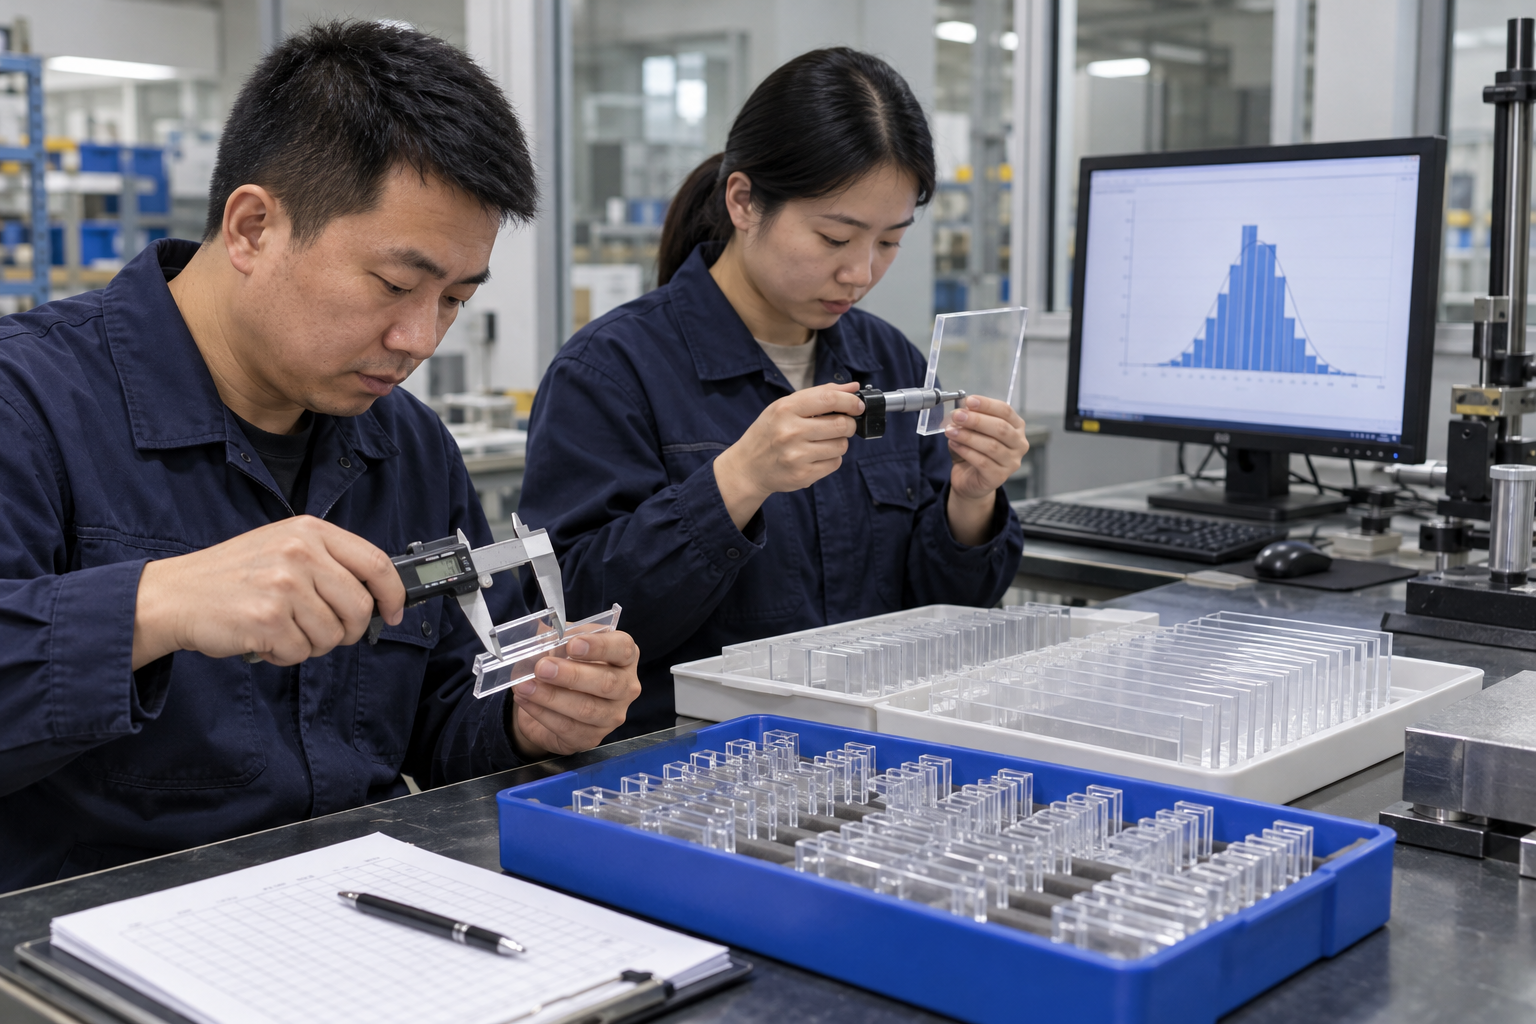
Show factory verification of Cp and Cpk capability study
- Placement
- after-second-section
- Caption
- Illustrative AI-generated photograph: Chinese technicians record production evidence for the approved Cp and Cpk capability study condition.
- ALT text
- Chinese technicians checking Cp and Cpk capability study during LED board production
View AI image direction
Use case: photorealistic-natural. Asset type: editorial photograph for a LumDigi B2B LED acrylic drawing board technical guide. Chinese adult QC technicians repeatedly measure panel thickness and base-slot width from time-ordered production samples and preserve raw observations for capability review. Landscape 3:2 composition, candid documentary commercial photography, natural modest lighting, realistic transparent acrylic, restrained plausible LED glow, genuine workshop or sample-room texture, believable anatomy. If employees appear, every employee is a Chinese/Asian adult. No invented logos, certification marks, readable documents, readable instrument values, numerical test results, watermark, or text overlay. This is an illustrative planning scene, not proof of an actual LumDigi test, factory result, shipment, or customer project.
Turn the article into a practical sourcing brief
Use the checkpoints above to document the product, evidence, packaging, and approval decisions relevant to your market. A clear brief helps suppliers respond to the same commercial question and gives your team a traceable basis for the next step.
Useful external references
- NIST: What is process capability?
Primary NIST explanation of process capability, specification limits, stable processes and Cp/Cpk indices.
- NIST: Process monitoring and control
NIST engineering-statistics guidance for monitoring process behavior and distinguishing common from special causes of variation.
Measurement Uncertainty in LED Drawing Board Acceptance Decisions
A sourcing guide to preventing false accept and false reject decisions when dimensions, power or other measured results sit close to a specification limit.
Read article
Gauge R&R for LED Board Panel and Base Dimensional Inspection
A buyer guide to checking whether thickness, slot and seating measurements are reliable enough to control fit across production.
Read article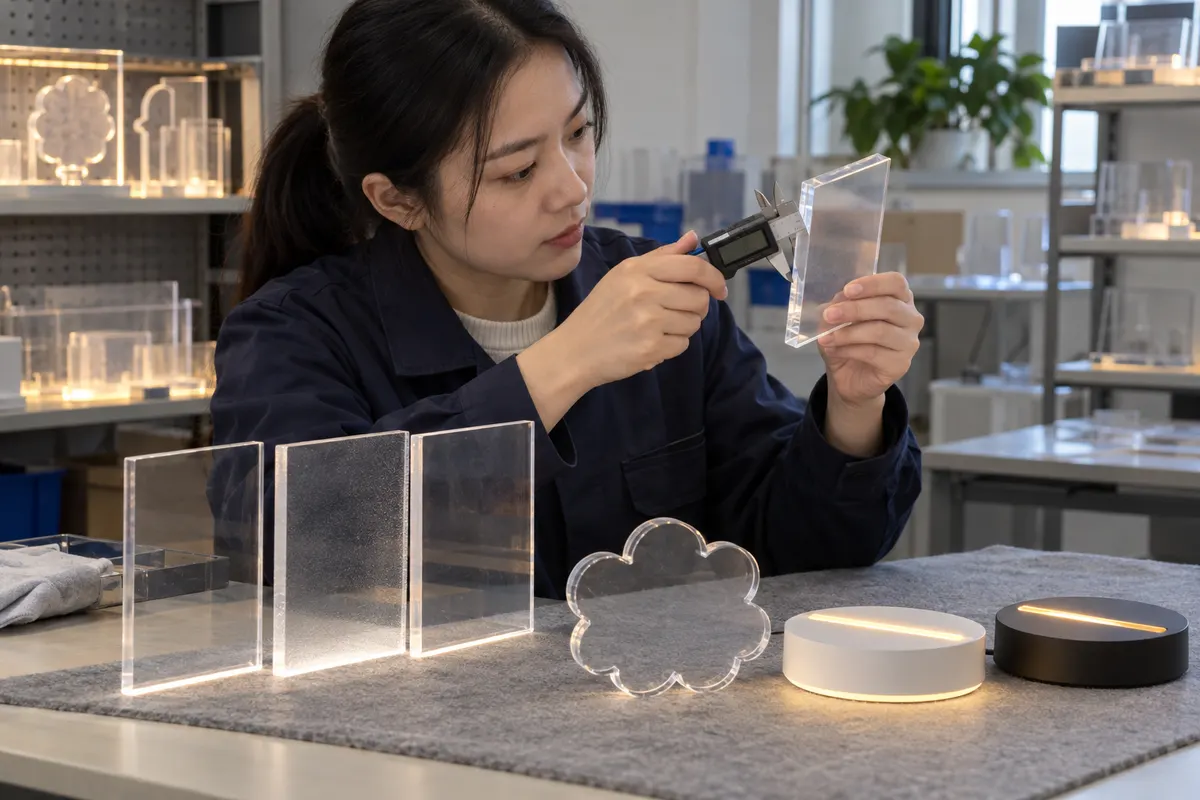
Acrylic Panel Thickness Tolerance and LED Board Base-Slot Fit
A tolerance-stack guide for preventing loose, tight or tilted panel fit in wholesale LED drawing-board bases.
Read article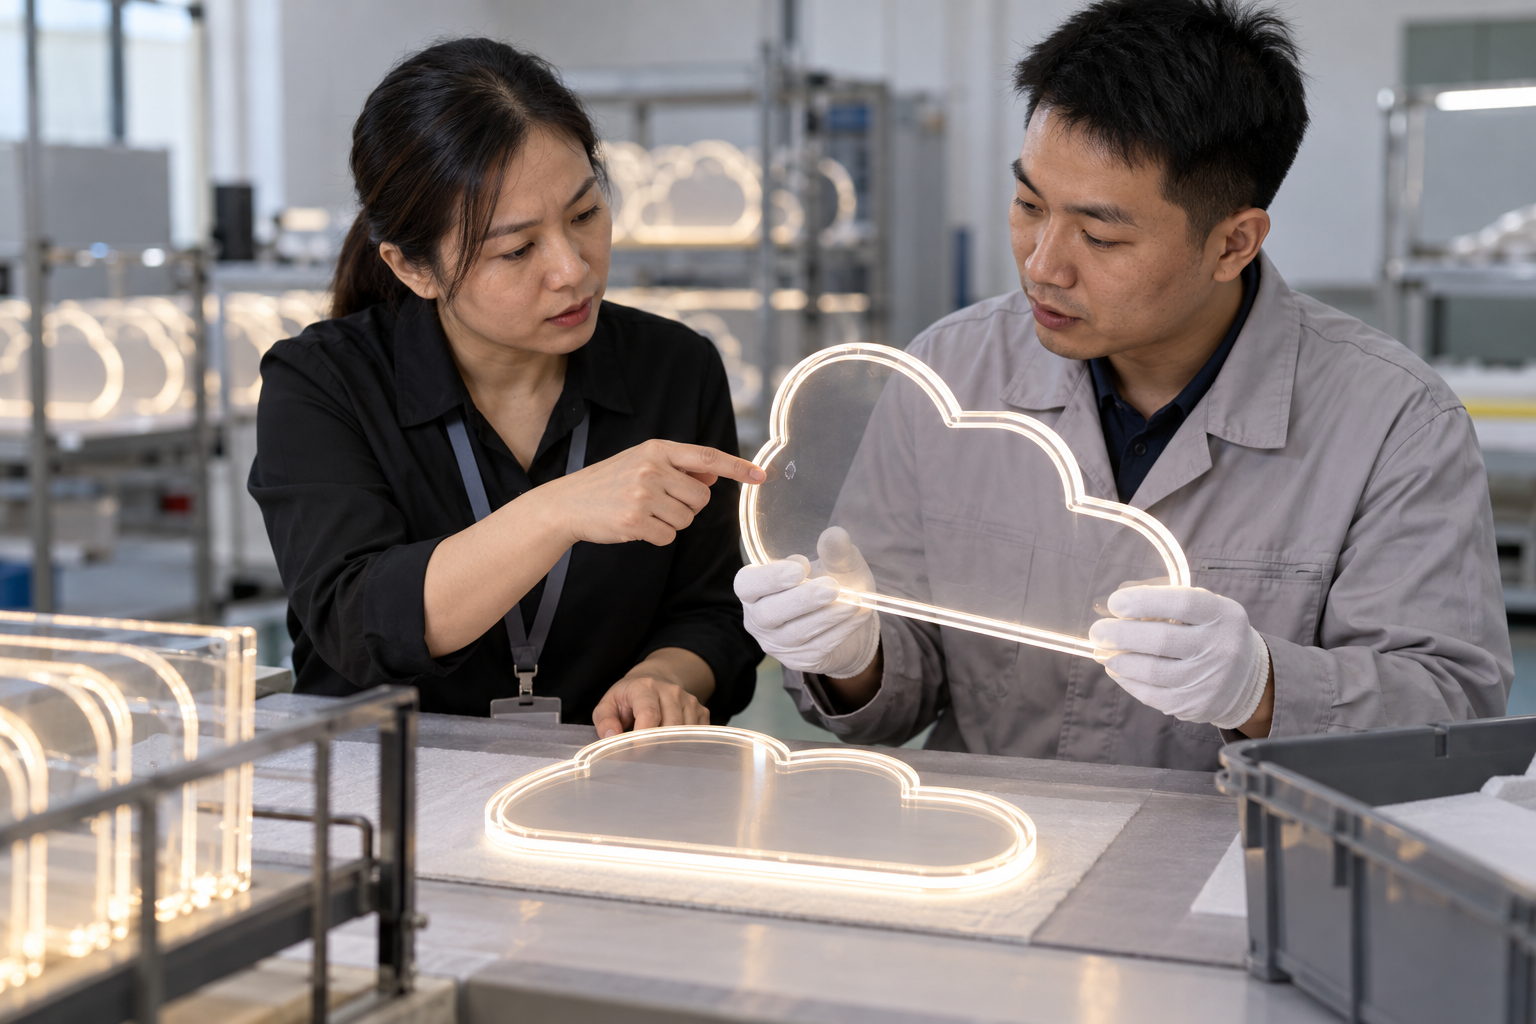
Deviation and Concession Control for LED Drawing Board Orders
A B2B guide to preventing temporary exceptions from becoming silent specification changes or recurring shipment disputes.
Read article