Inspect what the order actually specifies
A useful QC checklist references approved versions, defines observable checks, records findings clearly, and keeps formal technical requirements under the buyer's qualified process.
1. Build the inspection plan from controlled order documents
The checklist should cite the purchase reference, product specification, approved sample, artwork versions, set contents, packaging standard, and buyer-defined sampling or acceptance method.
Begin with an inspection cover sheet that identifies supplier, purchase reference, product and variant codes, quantity presented, inspection stage, location, date, and controlling document revisions. Attach or link the approved product drawing, sample identifier, bill of contents, appearance references, artwork register, pack instruction, and carton information. When these sources disagree, the inspector should flag the conflict rather than decide which informal message supersedes another.
Define the checks, method, result format, and authority before inspection. Distinguish a full count from a sampled observation and record the buyer's chosen sampling plan without presenting a generic plan as universally suitable. Identify critical release questions and escalation contacts. Formal safety, electrical, chemical, or market-compliance evaluation belongs to qualified processes and relevant evidence; a commercial visual and functional inspection supports but does not replace those responsibilities.
Convert the specification index into a working sequence before anyone reaches the line or finished-goods area. Put identity and quantity checks first, followed by visible parts, assembly, illumination, contents, retail pack, and shipping carton observations. For each checkpoint, state the document reference, tool or visual setup, units to be examined, result notation, and photograph required when a finding occurs. An inspector should be able to tell whether a dimension comes from the current drawing and whether an appearance judgment comes from a named sample photograph. Where the buyer has not supplied an acceptance rule, label the observation for buyer disposition instead of inventing one on site. This preparation keeps the checklist tied to the actual purchase file and prevents a convenient factory reference from silently replacing the agreed variant.
- Identify every product and artwork revision on the inspection cover sheet.
- Link observable checkpoints to the approved sample or written requirement.
- State the buyer-defined sampling and acceptance method before work begins.
- Define escalation owners for document conflicts and significant findings.
2. Check incoming acrylic panels and visible parts
Panel checks should cover identity, shape, dimensions, visible surfaces, edge treatment, decoration, protective film, and any defect zones defined by the buyer.
Confirm that the panel silhouette and dimensions match the current drawing and variant. Review front, rear, edges, cutouts, decorated areas, and base-contact zone under consistent lighting. Typical observations may include scratches, chips, haze, contamination, rough edges, warping, incorrect print placement, or protective-film damage, but the buyer must define what is acceptable for the product and viewing distance. Photographs should include scale and identify the sample or production unit.
Inspect bases, buttons, ports, cables or power components, markers, cleaning items, and printed pieces as separate incoming categories where relevant. Check color and finish against controlled references rather than memory or a screen capture. Keep findings tied to lot or time information available in the factory record. If rework is proposed, document the method and recheck result so a repaired surface is not assumed acceptable without evidence.
Panel review should follow the way the part moves through production. Check the protective film and label before removal, then examine both faces, cut perimeter, engraved or printed areas, base-contact edge, and any shaped tips that are easily knocked in trays. Photograph a defect with its location on the silhouette and with enough scale to distinguish a small speck from a long scratch. Separate contamination that can be cleaned from surface damage, and record whether rework changes the edge or decoration. For bases and accessories, keep findings under their own component references so a recurring color mismatch or damaged port area can be traced to the relevant material group. A mixed pile of rejected pieces is poor evidence because it does not show which variant, process stage, or incoming lot needs attention.
| Visible area | Observation method | Reference |
|---|---|---|
| Panel face | Consistent light, protected-film status, close and normal views | Approved appearance sample and defect criteria |
| Panel edge | Perimeter review and base-contact close-up | Drawing and edge-finish reference |
| Decoration | Position, orientation, color, adhesion or print appearance | Numbered artwork and approved sample |
| Base and accessories | Color, finish, identity, and obvious damage | Component list and controlled color reference |
3. Verify assembly, fit, controls, and illumination
Functional inspection should follow a repeatable sequence for panel seating, base stability, input connection, control behavior, lighting modes, and normal handling of the approved set.
Check that the correct panel fits the correct base in the intended orientation, seats to the approved depth, and presents consistently. Observe gaps, looseness, binding, exposed damage, or instability using defined methods. Connect the specified power arrangement and follow the approved control sequence. Record whether each expected mode operates and whether the sample used for comparison is the same product revision. Do not infer service life or electrical compliance from a short operational check.
Use an inspection drawing reference to mark the panel with every included fluorescent marker color and observe the lit presentation under a consistent environment. Confirm that controls remain usable during the check and that the set can be returned to its packed state. If the buyer specifies repeated operations or time-based checks, document the procedure, quantity, and actual observations. Any abnormal sound, heat, flicker, intermittent connection, or physical movement should be described factually and escalated under the inspection plan.
Use the same assembly script for every checked unit: identify the panel and base, inspect the contact areas, seat the panel without extra force, connect the specified power item, and operate controls in the recorded order. Mark the panel with the approved marker assortment using a repeatable small pattern so color and illumination can be compared without covering existing workmanship findings. Note whether a symptom appears immediately, only after reseating, or only in one control mode. If intermittent behavior occurs, preserve the unit identity and do not normalize it by repeated adjustment before recording the first observation. The checklist should capture what happened during the defined operation, not convert a brief factory check into a claim about durability, electrical performance, or long-term use.
- Match panel and base references before checking fit or function.
- Follow one documented power and control sequence across inspected units.
- Use the approved marker set and consistent viewing conditions.
- Describe abnormal observations without converting a brief check into a lifetime claim.
4. Verify accessories, printed materials, and set completeness
Every packed unit should be checked against the current bill of contents, with variants and optional items clearly separated to prevent omissions or mixed sets.
Create a visual component standard showing the panel, base, markers by quantity and color, power-related item, cleaning item, instructions, inserts, labels, and any buyer-approved accessory. Inspectors can then compare actual items without interpreting a generic product description. Check product and component identity, visible condition, placement, and retained quantity according to the plan. A present accessory may still be wrong if it belongs to another colorway or packaging revision.
Review printed content by revision and placement, not by a quick glance at the logo. Confirm product name, images, languages, identifiers, warnings or statements assigned through the buyer's review, and correspondence between insert and product. Scan or verify buyer-supplied barcodes through the method required by the buyer while avoiding claims beyond that check. Photograph a complete set and any discrepancy in a way that shows both the item and the unit or carton context.
Set-completeness inspection works best with a photographed master flat lay for each retail variant. Open the selected unit, arrange the acrylic panel, base, markers, cleaning item, power-related component, instructions, inserts, and any promotional piece in the same order, then compare count, color, code, condition, and packing position. Printed materials need their own revision check because a physically complete set can still carry instructions or imagery for another shape. When a carton contains mixed language versions, record how unit and carton labels distinguish them and sample from each group. Missing low-cost accessories should not be merged into a general packaging note; they affect what the customer receives and should be reported by item and affected quantity.
| Set element | Completeness control |
|---|---|
| Markers | Approved count, color assortment, condition, and packing position |
| Power-related component | Correct type for the specified set and destination review |
| Cleaning or care item | Presence, identity, and match to instructions |
| Printed material | Current product, language, revision, and pack placement |
5. Inspect retail packaging and shipping cartons
Packaging checks should connect structural protection, artwork identity, component placement, retail finish, carton count, marks, sealing, and actual measured shipment data.
Open selected units layer by layer and compare the arrangement with the approved packed sample or packing instruction. Check whether the panel, base, markers, and accessories are retained, separated from harmful contact, and presented in the intended sequence. Observe retail-carton damage, print alignment, color direction, closures, labels, and contamination against buyer-defined criteria. After review, confirm the set can be repacked consistently rather than forcing components into an unsuitable insert.
For shipping cartons, record product and variant mix, units per carton, inner pack if used, marks, label information, carton dimensions, measured weight, sealing method, and visible condition. Compare results with the approved logistics record and note the measurement equipment or method. If the buyer requires transport testing or a defined packaging validation, handle it through the separate agreed procedure; a carton appearance inspection alone cannot establish distribution performance.
Open selected shipping cartons layer by layer and retain the sequence in photographs before moving components. Review whether the retail cartons face the approved direction, whether acrylic edges contact another hard part, whether marker packs remain in their intended pocket, and whether the insert shows crushing, tearing, or evidence of forced closure. Compare retail print with the artwork register and then record shipping marks, pack count, carton dimensions, weight, sealing, and visible condition using the agreed equipment. If an inner arrangement differs from the packed sample, describe the actual positions rather than calling the pack merely 'different.' Transport testing, if required by the buyer, remains a separate defined activity; carton appearance at inspection cannot establish how the shipment will perform in distribution.
- Compare layer-by-layer packing with the approved packed sample.
- Match retail artwork, labels, and variant identity to current files.
- Record actual carton pack count, marks, dimensions, weight, and seal.
- Separate visual carton review from any formal transport-test requirement.
6. Report findings and control shipment release
The report should show inspected scope, evidence, finding severity under the buyer's rules, affected quantity, corrective action, recheck result, and the authorized release decision.
Write each finding with product reference, location, quantity observed, requirement, actual condition, and clear images. Grouping unlike defects under 'quality issue' makes corrective action difficult. Use the buyer's approved classification and acceptance rules, and keep raw observations available. If the supplier disputes a finding, record the evidence and decision trail. Corrected units should be distinguishable from unchecked goods where the agreed process requires it.
The inspection result informs but does not automatically make the commercial release decision. The authorized buyer reviews the report, open documentation, concessions, rework evidence, reinspection scope, and shipment status. Possible outcomes should be named according to the buyer's process rather than implied by a pass label. Archive the final report with the purchase and specification records so later customer-service, reorder, and supplier-review discussions can use the actual order evidence.
Write each finding as a traceable record: requirement, observed condition, product or carton identity, inspected quantity, affected quantity known at that moment, photographs, supplier response, and buyer disposition. Keep cosmetic acrylic findings separate from missing contents, artwork errors, and functional observations because they may require different corrections and release decisions. When the factory reworks goods during the visit, state exactly which units were rechecked and whether unopened stock remains outside that evidence. The final summary should show limitations, unresolved document conflicts, concessions, and any requested follow-up instead of reducing the visit to a colored pass badge. Shipment release belongs to the authorized buyer after inspection evidence is considered alongside other technical, commercial, and documentation requirements.
- Describe requirement, observation, affected scope, and evidence for each finding.
- Record corrective action, responsible party, and recheck method.
- Keep concessions and release authority traceable to the buyer's process.
- Archive the report with specification, artwork, and shipment records.
Frequently asked questions
What belongs on an LED drawing board QC checklist?
Include document identity, product and variant verification, acrylic and base workmanship, assembly and fit, controls and illumination, marker interaction, set completeness, printed materials, retail pack, shipping cartons, findings, corrective action, and release authority. Adapt methods to the order.
Can a pre-shipment inspection prove product compliance?
A commercial inspection can verify defined visible, functional, quantity, and packaging checkpoints. It does not replace the buyer's technical, laboratory, legal, or market-specific compliance processes. Those requirements need qualified review and appropriate evidence.
How should defects be reported?
Identify the product, location, requirement, actual observation, affected scope, and images. Use the buyer's defined classification instead of vague labels. Record corrective action, recheck results, concessions, and the person authorized to make the final disposition.
Why reference an approved sample during inspection?
A labelled sample can clarify appearance and presentation that written text alone may not express. It should be used with current drawings and specifications, not as a substitute for them, and its identifier must be traceable to the order.
Image planning for this topic
These notes document the role and intended context of the two visuals used in this guide.
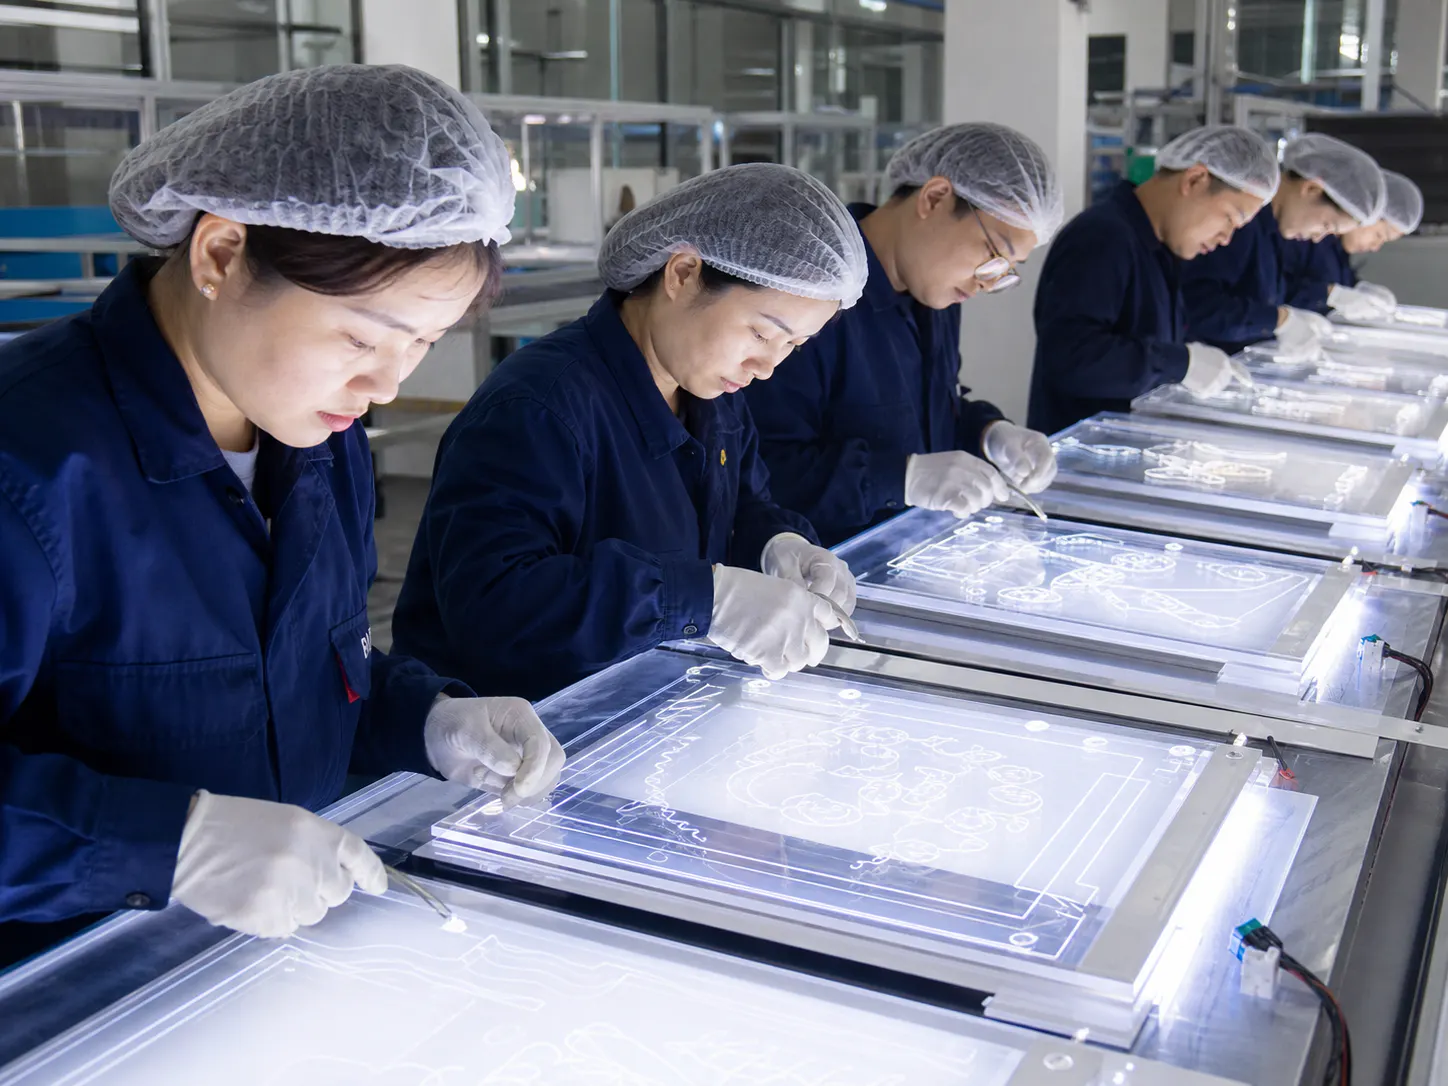
Show an organized commercial QC workflow for illuminated drawing boards.
- Placement
- hero
- Caption
- LED drawing boards are checked against product and packing references before release.
- ALT text
- Chinese quality inspectors checking LED drawing boards at a factory station
View AI image direction
Photorealistic documentary image of a Chinese LED drawing-board factory quality station with twelve Chinese inspectors checking clear acrylic panels, shaped bases, control functions, fluorescent marker sets, and numbered inspection sheets, understated LumDigi logos on uniforms and sample cards, realistic industrial lighting and equipment, organized work-in-process, no competitor brands, no exaggerated clean-room styling, wide editorial composition.
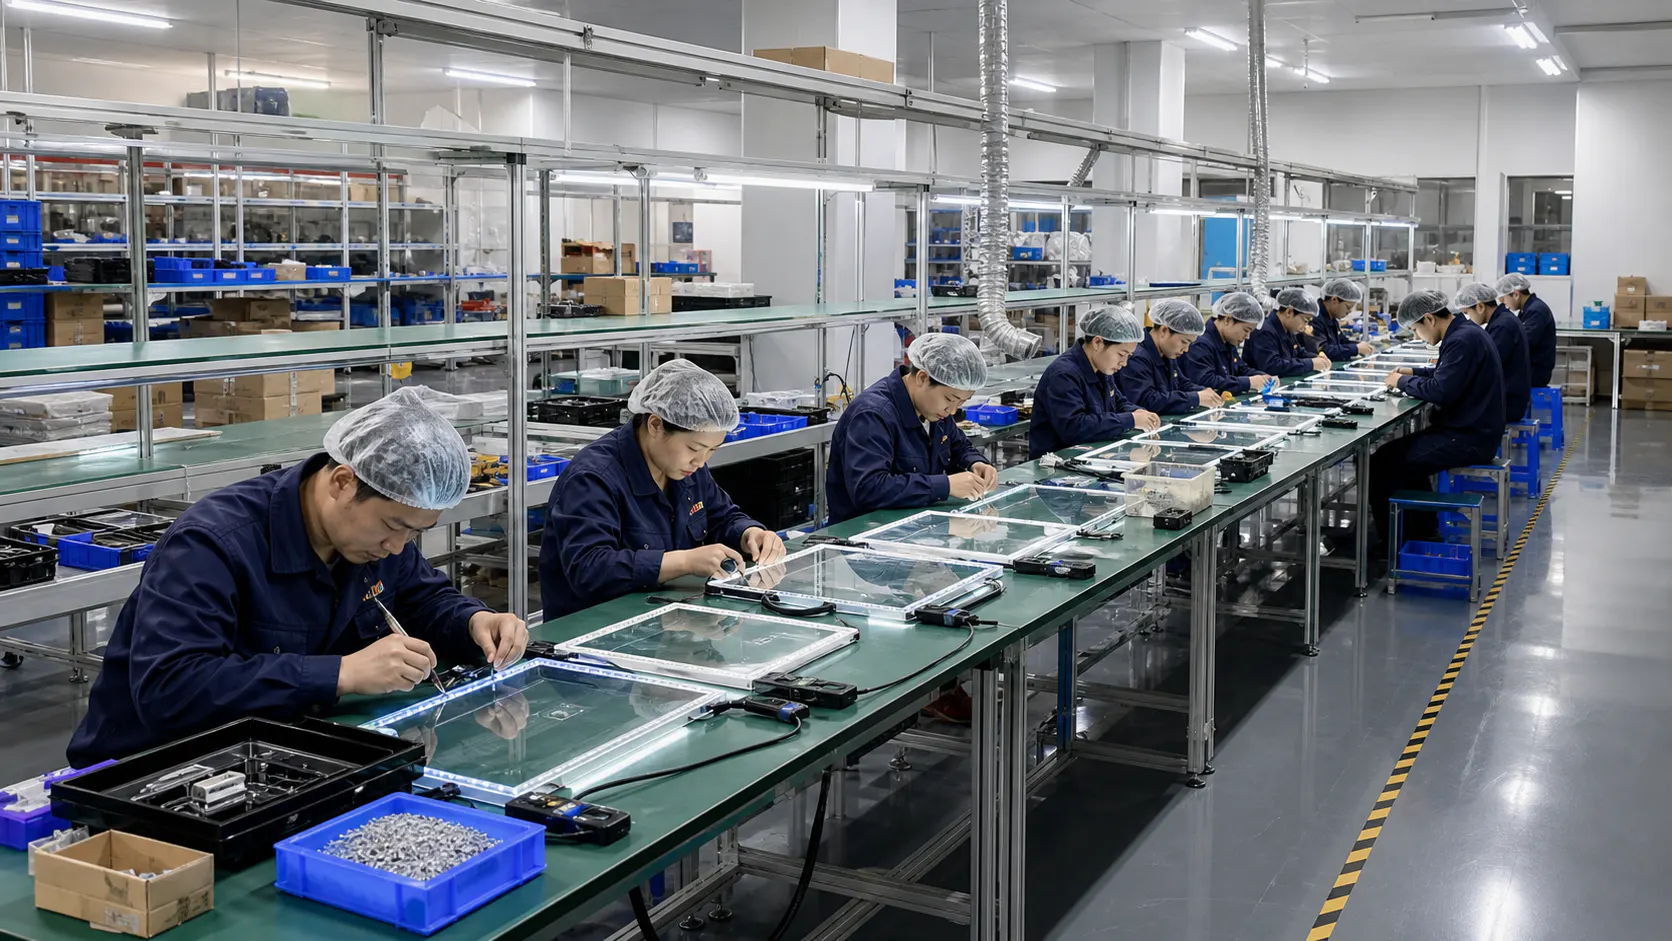
Illustrate assembly and in-process fit checks before final packing.
- Placement
- after-key-considerations
- Caption
- In-process checks make panel-to-base and component issues visible before packing.
- ALT text
- Chinese workers assembling shaped acrylic LED fluorescent boards
View AI image direction
Realistic factory photography showing ten to fifteen Chinese workers assembling varied shaped acrylic LED fluorescent drawing boards at orderly benches, workers checking panel seating, base connections, control buttons, and component identity, subtle LumDigi badge on neutral uniforms, authentic hand tools and production trays, balanced natural overhead light, candid documentary perspective, no competitor branding or invented certification signs.
Turn the article into a practical sourcing brief
Use the checkpoints above to document the product, evidence, packaging, and approval decisions relevant to your market. A clear brief helps suppliers respond to the same commercial question and gives your team a traceable basis for the next step.
Useful external references
- GS1 Product Image Standard
Primary guidance for consistent product-image identification and digital assets.
- CPSC business and manufacturing resources
Official U.S. business resource; destination-specific obligations need suitable qualified review.
Pre-Shipment Inspection for Acrylic LED Drawing Boards
Use a production-specific inspection plan to verify the ordered configuration and provide the buyer with traceable evidence before shipment release.
Read article
LED Fluorescent Boards for Wholesale: A Buyer's Sourcing Checklist
Turn a promising illuminated drawing-board sample into a clearly specified, reviewable wholesale project with this buyer-focused sourcing checklist.
Read article
LED Drawing Board Freight Protection Guide: Reducing Transit Damage Risk
A practical B2B guide for buyers preparing retail-ready orders for international transport who need to identify packaging and shipment questions that reduce avoidable transit risk for acrylic panels, bases, accessories, and printed retail packs.
Read article
How to Build a LED Drawing Board Product Specification Sheet
A practical B2B guide for B2B teams aligning suppliers, quality reviewers, packaging teams, and sales channels who need to create one readable source of truth for the exact board configuration, set contents, packaging, and verification requirements.
Read article