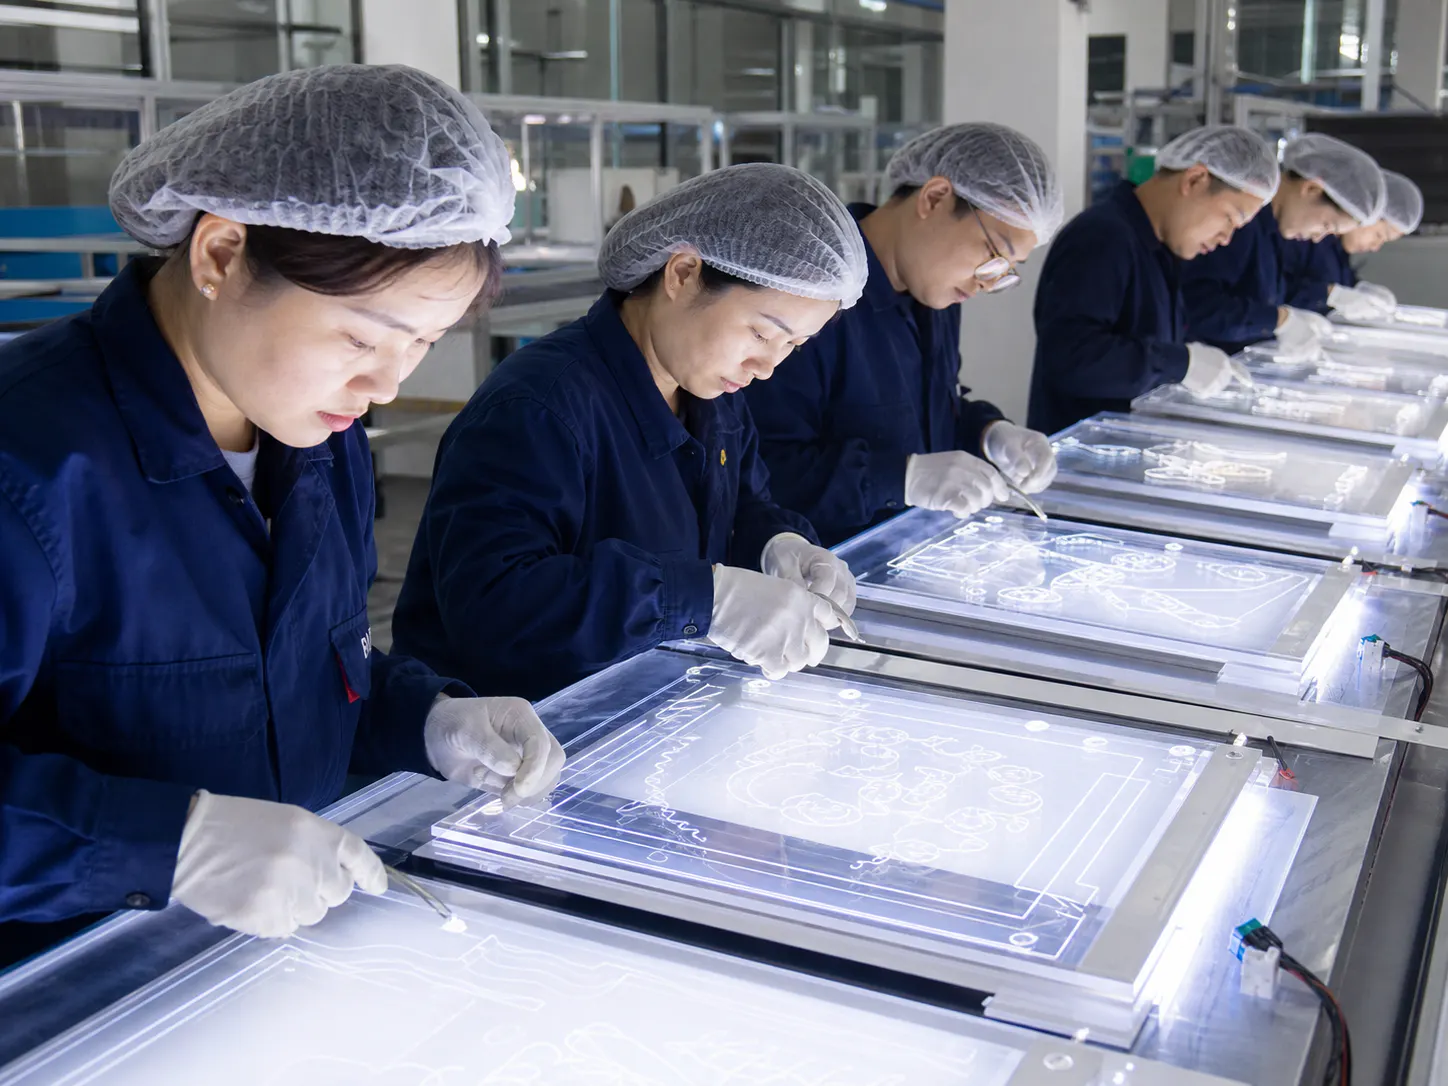
Make shipment release an evidence-based decision
A pre-shipment inspection identifies the presented order, follows buyer-defined methods, records product and packing observations, and routes findings to authorized disposition without replacing formal compliance work.
1. Confirm readiness, scope, and inspection basis
Before arrival, confirm goods presented, packing status, product variants, document revisions, sampling instructions, checkpoints, and people authorized to resolve conflicts.
The inspector needs the purchase reference, quantity by variant, factory location, readiness statement, current specification, sample code, artwork index, contents list, packing standard, carton data, and buyer-approved inspection instruction. Confirm whether goods are finished and packed to the planned extent. If presentation differs, record it and obtain direction; changing scope during inspection can make results misleading.
Confirm the inspection presentation in writing on the day before the visit and again on arrival. Reconcile finished units and packed cartons by variant against the booking, note any goods still in assembly or rework, and identify the physical area where selections can be made without factory pre-sorting. Review the inspection file for the latest product drawings, sample codes, artwork PDFs, contents list, packing reference, and buyer instructions. If the available quantity or packing stage differs materially, pause and obtain buyer direction before changing the planned method. The report should preserve that limitation because results from a partial or specially prepared presentation cannot automatically describe goods that were not available. Clear readiness evidence protects both buyer and factory from a misleading inspection conclusion.
- Verify order, variant quantities, location, and readiness status.
- Issue current specifications, artwork, pack, and sample references.
- State buyer-defined sampling and acceptance instructions.
- Name escalation and disposition contacts before inspection.
2. Verify product identity, variant mix, and quantity
Count or reconcile cartons and units according to the plan, then match product, package, and carton identifiers across every presented shape or color.
Compare carton marks, labels, retail pack, base or product markings, panel silhouette, and contents with the purchase variant matrix. Record actual presented quantities, selected cartons, and mixed-carton structure. Do not assume a similar shape is an approved substitute. Photograph identifiers and note missing, duplicated, damaged, or inconsistent labels in their carton context.
Start at the shipping-carton level and trace selected units inward. Record carton numbers or locations, marks, stated pack count, variant label, retail artwork, product marking, acrylic silhouette, base color, and component codes in one selection sheet. For mixed cartons, document the arrangement and select across the relevant positions rather than checking only the easiest layer. Reconcile presented counts with the purchase matrix while keeping damaged or held cartons visible in the summary. A similar-looking star, cloud, or animal shape must never be treated as interchangeable without an approved variant reference. These identity checks give later workmanship and function observations a reliable denominator: reviewers can see exactly which units and versions were examined instead of receiving photographs detached from the shipment structure.
When quantities are reported from factory records, distinguish documented reconciliation from a physical count performed during the visit. Note pallets, sealed cartons, loose retail units, and any stock excluded from presentation so the total is not mistaken for one uniform verification method. If labels are replaced during inspection, retain before-and-after photographs and record which cartons received the correction. The final quantity table should show what was presented, what was selected, what discrepancy was observed, and what evidence supports any corrected figure, allowing the buyer to judge the shipment identity without an unexplained total.
| Level | Identity evidence |
|---|---|
| Shipment | Order and quantity summary |
| Shipping carton | Marks, label, pack count, variant |
| Retail unit | Artwork, product code, shape, color |
| Components | Panel, base, markers, inserts, accessories |
3. Inspect acrylic workmanship, fit, controls, and lit presentation
Use controlled references and repeatable observations for panel faces and edges, base finish, seating, controls, connection, illumination modes, and marker drawing.
Check visible surfaces under consistent light, noting protective-film status. Observe scratches, chips, haze, contamination, edge finish, print or decoration, base color and joints against buyer criteria. Seat the correct panel, use the specified power arrangement, follow the control sequence, and draw with the approved marker set. Record actual behavior without extrapolating a short check into service-life or compliance claims.
For each selected unit, record protective-film status before judging acrylic surfaces, inspect faces and edges under the agreed light, and compare decoration, base finish, controls, and seating with the approved references. Use the defined power arrangement and control sequence, then make a small repeatable drawing with every included marker color and photograph the lit presentation in a consistent setting. Preserve unit identity when flicker, intermittent contact, unusual movement, visible damage, or another observation occurs; do not keep reseating the panel until the initial symptom disappears from the record. A pre-shipment function check reports behavior during the stated procedure. It should not be presented as evidence of service life, formal safety, or destination compliance, which require separate qualified methods and review.
- Identify protective-film condition before judging panel surfaces.
- Check panel-to-base fit for each inspected variant.
- Follow one documented control and illumination sequence.
- Photograph findings with unit, location, and scale context.
4. Check set contents, artwork, and printed information
Compare every unit with the current bill of contents and confirm that printed materials belong to the product, language, and artwork revision packed.
Lay out panel, base, markers, power-related item, cleaning accessory, instructions, inserts, and other approved pieces. Confirm quantities, color assortment, condition, and pack placement. Compare retail panels and printed documents with numbered files, including buyer-supplied identifiers and product imagery. Route technical or market claims through the buyer's separate evidence review rather than judging them from print presence.
Open retail units from more than one selected carton and create a labelled flat lay for each variant. Count the panel, base, marker colors, cleaning item, power-related component, instructions, inserts, labels, and any promotion piece against the current bill of contents. Compare product photographs and callouts on every carton panel with the physical set, then verify language and identifiers against the artwork register. A set can be physically complete yet informationally wrong if it carries an insert for another control sequence or a side-panel image of another shape. Report missing items, wrong items, obsolete files, and mixed versions as separate findings so correction evidence can show exactly what was repacked or replaced before the buyer considers release.
| Check | Mismatch to prevent |
|---|---|
| Contents | Missing, extra, wrong-color, or wrong-variant pieces |
| Artwork | Obsolete file or image of another configuration |
| Language | Incorrect insert or mixed destination version |
| Identifiers | Retail, product, and carton codes that do not align |
5. Inspect inner protection, retail packs, and shipping cartons
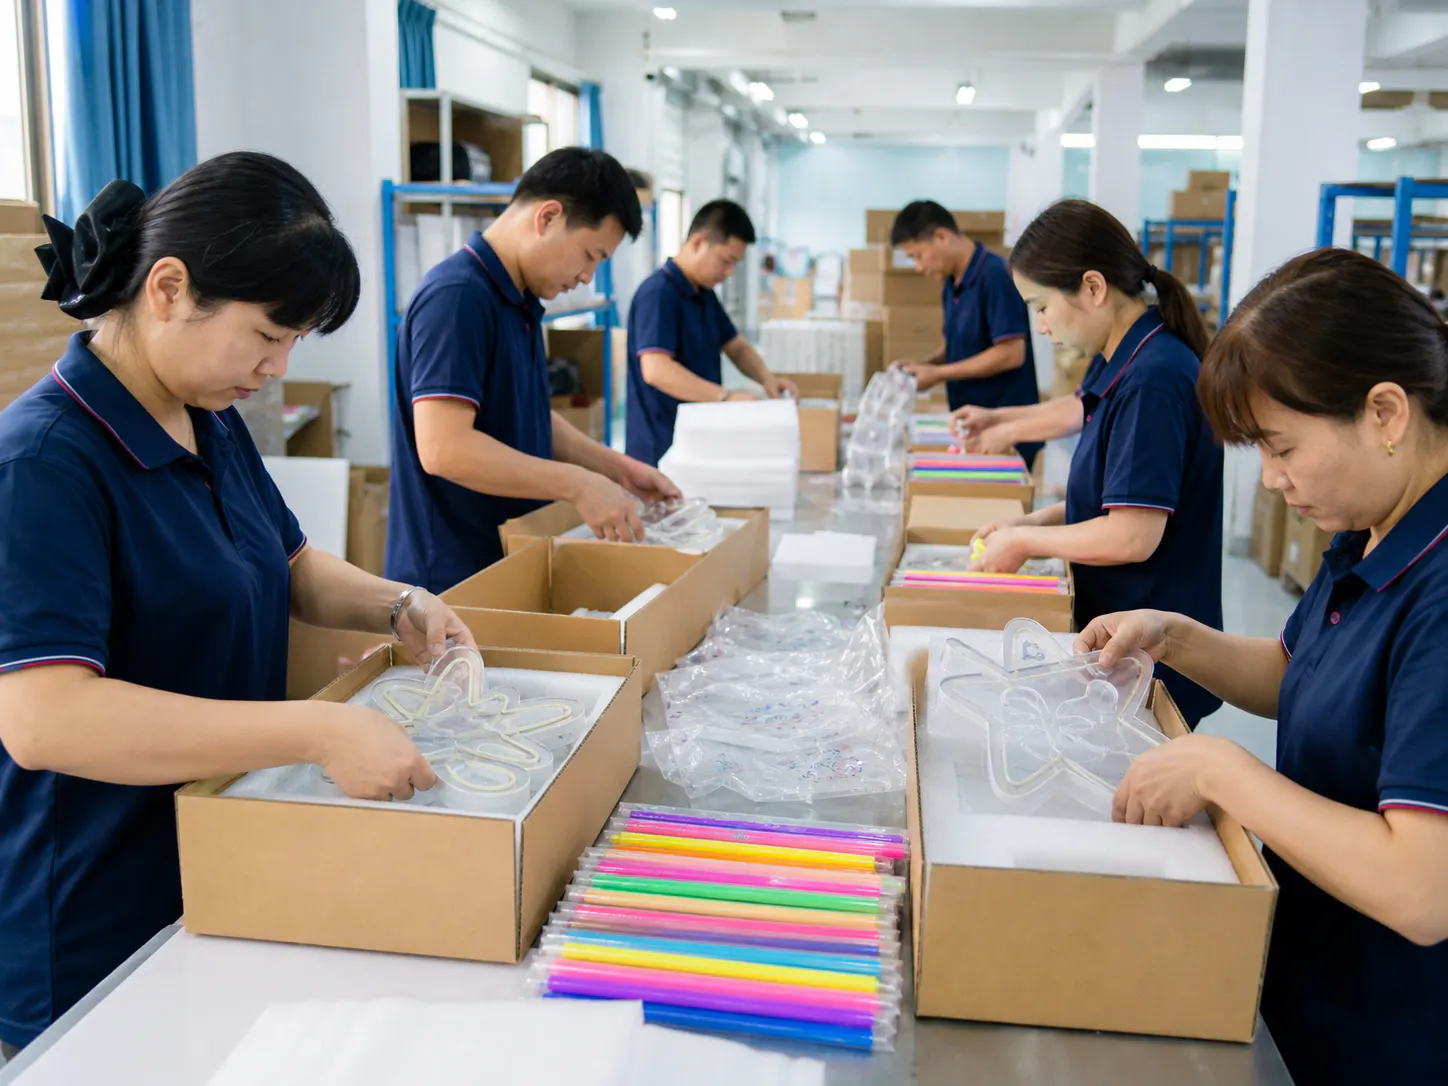
Open selected cartons through every layer, verify component retention and retail finish, then record actual carton count, marks, dimensions, weight, sealing, and condition.
Compare the inner arrangement with the approved packed sample, looking for uncontrolled movement, acrylic contact, misplaced accessories, crushed inserts, or forced repacking. Review retail print, closures, labels, and cleanliness. Measure cartons using the agreed method and record equipment. If the order requires transport validation, treat it as a separate defined process; visible carton condition alone does not establish performance.
Photograph the unopened shipping carton and seal before removing layers, then capture retail-carton orientation, void fill, insert positions, acrylic edge protection, accessory pockets, and the sequence needed to reach the product. Compare actual packing with the approved sample and look for movement marks, crushed supports, hard-part contact, loose marker packs, contamination, or forced retail closure. Measure carton dimensions and weight using recorded equipment and verify pack count, marks, labels, and destination information supplied by the buyer. If corrections are made, request images or reinspection evidence from newly packed cartons rather than only the demonstration unit. Visual inspection documents the presented pack; any transport-test requirement remains a separate buyer-defined process with its own method and acceptance decision.
- Photograph unpacking sequence and component positions.
- Check retail finish against buyer-defined acceptance criteria.
- Record actual carton pack, dimensions, weight, marks, and seal.
- Keep transport-test requirements separate from visual inspection.
6. Turn inspection findings into an authorized release decision
A complete report states scope and limitations, results by checkpoint, finding evidence, affected quantity, correction, reinspection, open documents, and buyer-authorized disposition.
Describe each finding against its requirement and avoid grouping unlike issues. Record supplier comments separately from inspector observations. If corrections occur, define which goods were rechecked and how. The buyer then considers inspection evidence alongside technical documents, concessions, payment terms, and shipping status. Archive the release decision with the order so later review is grounded in facts rather than a simple pass or fail label.
Organize the report so the authorized buyer can trace each conclusion back to scope and evidence. Begin with presented quantities, selection details, document revisions, methods, and limitations, then show results by identity, workmanship, function, contents, artwork, retail pack, and shipping carton. Each finding should cite the requirement, unit or carton reference, known affected quantity, photographs, factory comment, correction, and recheck status. Separate unresolved documentation from physical observations and make clear which stock was not examined after rework. The final page should list open decisions without turning them into an inspector's commercial approval. The buyer can then release, hold, accept a documented concession, or request further action while preserving the reasoning and evidence with the shipment record.
Archive raw photographs with filenames that retain carton or unit references rather than relying only on compressed report pages. Store the selected-carton list, count sheets, equipment notes, revised evidence supplied after the visit, and the buyer's signed disposition under the shipment reference. If the decision is conditional, state who will verify the outstanding correction and which stock it covers. This archive gives receiving or later sourcing teams enough context to distinguish a shipment-specific observation from a recurring specification issue, and it prevents a one-word result from becoming the only record used for the next order.
- State inspection scope, limitations, and exact document revisions.
- Link findings to requirements, quantities, photographs, and disposition.
- Document rework and reinspection scope instead of assuming closure.
- Keep shipment release with the buyer's authorized decision maker.
Frequently asked questions
When should pre-shipment inspection occur?
Book it when enough of the identified order is finished and packed for the agreed scope. Confirm readiness, quantity, and packing status before arrival and record limitations if actual presentation differs.
What should inspectors check on acrylic LED boards?
Typical commercial checks cover identity, quantity, panel and base workmanship, fit, controls, illumination, marker interaction, contents, artwork, retail packing, carton data, findings, and correction evidence under buyer-defined methods.
Does pre-shipment inspection replace laboratory or compliance work?
No. It provides commercial product, quantity, function, and packaging evidence for defined checkpoints. Technical, legal, laboratory, and destination-market responsibilities require their own qualified review.
Who decides whether a shipment is released?
The buyer's authorized decision maker reviews the inspection, documents, concessions, corrective action, commercial status, and open risk. An inspector reports evidence according to instructions; release authority should be explicit.
Image planning for this topic
These notes document the role and intended context of the two visuals used in this guide.
Show traceable pre-shipment product inspection.
- Placement
- hero
- Caption
- Structured inspection evidence supports the buyer's shipment-release decision.
- ALT text
- Chinese inspectors checking acrylic LED boards before shipment
View AI image direction
Realistic documentary photograph of a pre-shipment inspection in a Chinese LED drawing-board factory, Chinese inspectors comparing shaped acrylic panels, bases, illuminated function, marker contents, and numbered specifications at a QC table, subtle LumDigi marks on sample cards and uniforms, authentic cartons and measurement tools, natural factory light, no competitor logos or invented compliance badges.
Show carton, packed-set, and label verification.
- Placement
- after-key-considerations
- Caption
- Shipment inspection connects retail presentation with carton identity and logistics data.
- ALT text
- Chinese workers and inspector checking packed LED board cartons
View AI image direction
High-detail Chinese factory packing area with ten Chinese workers and one Chinese inspector opening selected cartons of shaped LED fluorescent boards, checking retail packs, inserts, carton marks, dimensions and weight against a clipboard, understated LumDigi carton print, realistic scales and tape measures, candid industrial photography, no competitor branding, no staged celebration.
Turn the article into a practical sourcing brief
Use the checkpoints above to document the product, evidence, packaging, and approval decisions relevant to your market. A clear brief helps suppliers respond to the same commercial question and gives your team a traceable basis for the next step.
Useful external references
- GS1 Product Image Standard
Primary guidance for consistent product-image identification and digital assets.
- CPSC business and manufacturing resources
Official U.S. business resource; destination-specific obligations need suitable qualified review.
LED Drawing Board Quality Control Checklist Before Shipment
Convert the approved sample and order specification into a practical inspection plan covering product identity, visible workmanship, function, contents, packaging, and reporting.
Read article
LED Fluorescent Boards for Wholesale: A Buyer's Sourcing Checklist
Turn a promising illuminated drawing-board sample into a clearly specified, reviewable wholesale project with this buyer-focused sourcing checklist.
Read article
Fluorescent Marker and Acrylic Panel Compatibility: A B2B Sample Review Protocol
A sample-testing plan for buyers qualifying a specific marker formulation with a specific acrylic surface and care method.
Read article
Gift-Ready LED Drawing Boards: Packaging and Seasonal Planning
Create a gift proposition that protects the acrylic set, communicates the occasion, and remains controllable through artwork, packing, shipment, and seasonal change.
Read article